 Skip to content
Supporting Chocolate Manufacturing in the Heart of Suffolk
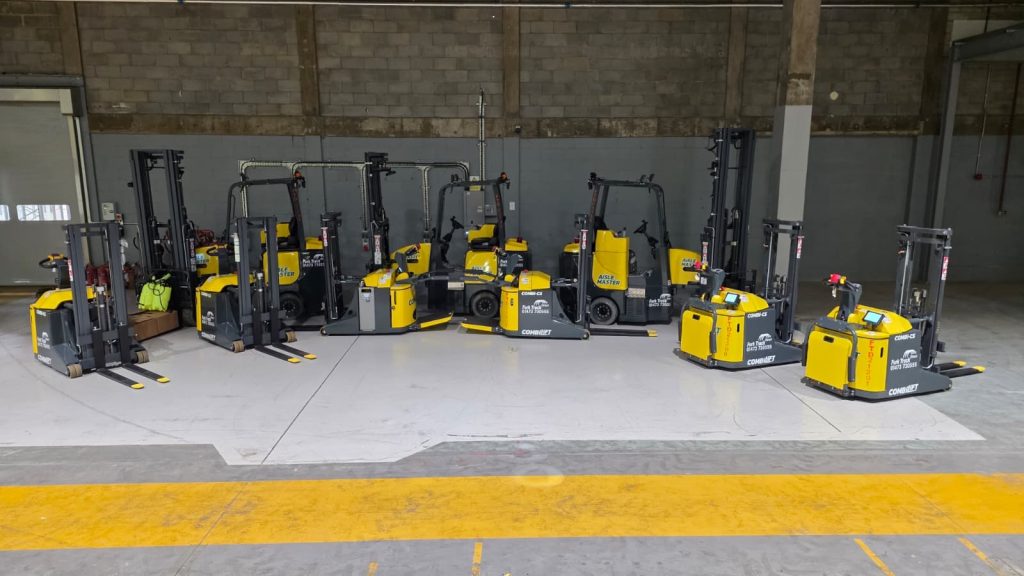
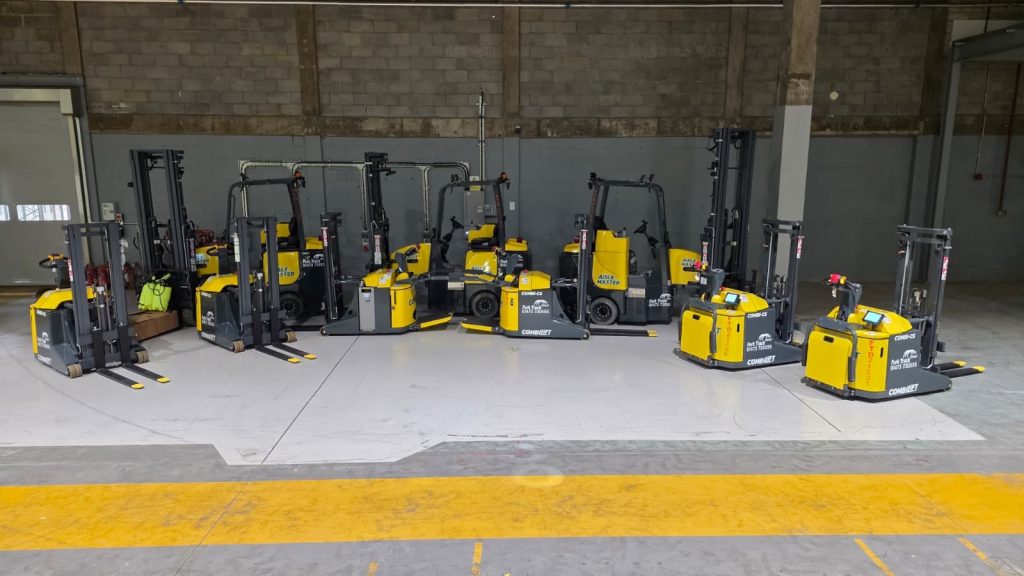
Fork Truck Direct is pleased to support GCB Cocoa UK with a comprehensive new materials handling fleet at its purpose-built chocolate manufacturing facility in Glemsford, Suffolk. The latest delivery includes three Aisle Master articulated forklifts and six Combilift CS pedestrian stackers, providing GCB Cocoa UK with a versatile combination of equipment designed to support product movement, storage and day-to-day operations across its manufacturing and warehousing environment. The fleet is also supported by GemOne Sapphire fleet management technology, providing GCB Cocoa UK with greater visibility over its materials handling operation alongside additional safety and compliance capabilities.
GCB Cocoa UK: British Chocolate Manufacturing in Suffolk
Part of the wider GCB Cocoa Group, GCB Cocoa UK operates a modern, purpose-built manufacturing facility in Glemsford, where the company produces an extensive range of solid and liquid chocolate products and supplies cocoa ingredients to customers across the UK food industry. The Suffolk facility combines traditional chocolate manufacturing processes with modern production technology and produces GCB’s Favorich range of milk, dark and white chocolates. Its capabilities also include a fully segregated dairy-free production line and a purpose-built pilot facility supporting new product development. GCB supplies customers across confectionery, bakery, snacking, cereals and gourmet markets, as well as industries including dairy, ice cream, beverages and food distribution.
With ingredients, finished products and outbound stock continually moving through the facility, efficient materials handling plays an important role in supporting the site’s manufacturing and storage operations.
Three Aisle Master Forklifts Maximise Storage Space
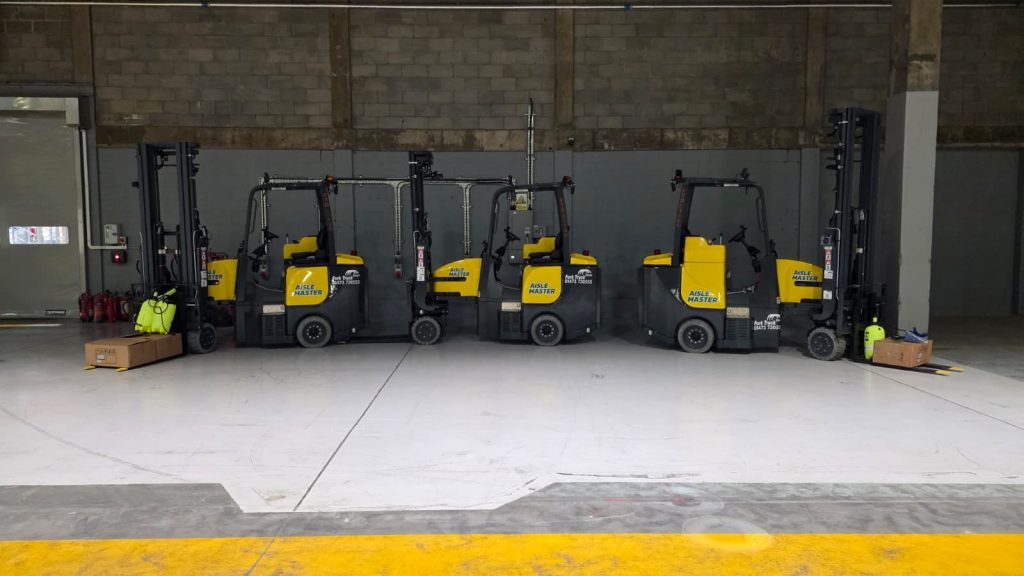
At the centre of the new fleet are three 1,500kg-capacity Aisle Master articulated forklifts, selected to provide efficient pallet handling while making maximum use of GCB Cocoa UK’s available warehouse space. Two trucks have been specified with 5,500mm triplex masts, while the third features a 6,350mm triplex mast, providing the lift capability required to access the site’s racking. Each Aisle Master is powered by a 775Ah 48V battery with three-phase charging and equipped with three LED work lights, front and rear blue safety spotlights and a white-noise reversing alarm.
The articulated design is particularly suited to GCB Cocoa UK’s operation. Aisle Master trucks are engineered to operate within very narrow aisles, allowing businesses to reduce the space required between racking and make more effective use of available storage capacity. Within the Glemsford facility, the trucks will support the movement of inbound ingredients and outbound stock, while enabling ingredients and finished products to be stored efficiently within the site’s narrow-aisle racking.
Six Combilift CS Stackers Support Factory-Floor Material Movement
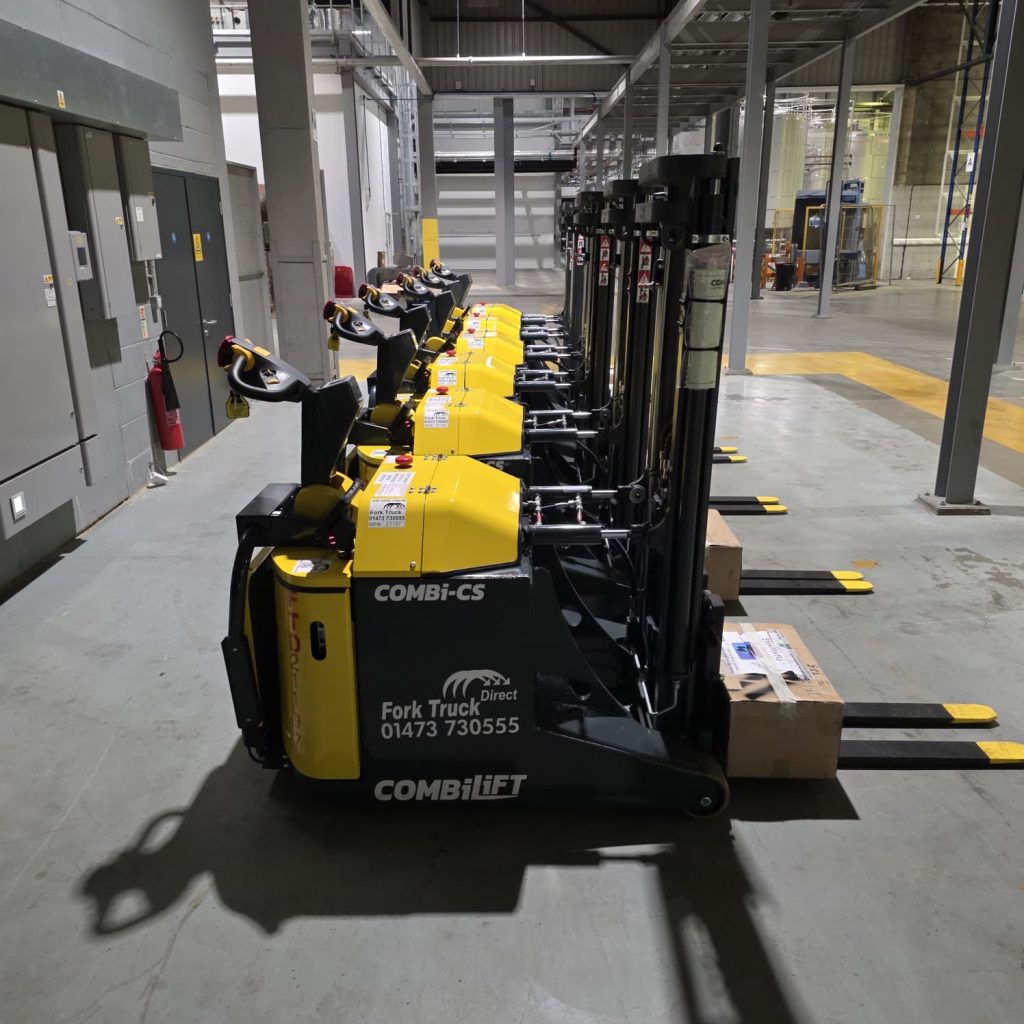
Complementing the Aisle Master fleet are six Combilift CS electric pedestrian stackers, providing a compact solution for lower-level material movement throughout GCB Cocoa UK’s production and storage areas. Each truck offers a 1,250kg capacity with a 2,450mm duplex mast and is powered by a 24V 360Ah lithium battery. The machines have also been specified with operator safety arms, white-noise reversing alarms and quartz rear drive wheels. Their compact design makes the Combilift CS particularly well suited to environments, where manoeuvrability and efficient use of floor space are important. Combilift’s patented multi-position tiller system allows the operator to remain to the side of the machine, providing visibility of the load and surrounding area while helping keep the operator away from the rear crush zone in confined spaces.
For GCB Cocoa UK, the six trucks will provide a reliable platform for moving materials throughout the factory and storage areas, working alongside the Aisle Master fleet to keep ingredients, products and stock moving efficiently through the operation.
GemOne Sapphire Brings Fleet Management and Safety Together
The project extends beyond the trucks themselves, with the fleet incorporating GemOne Sapphire technology to provide GCB Cocoa UK with a comprehensive fleet management and compliance solution. The system includes an in-truck touchscreen, web-based fleet management interface and impact monitoring, giving the business greater visibility and control over the operation of its materials handling equipment.The installation also incorporates AI-assisted front and rear pedestrian detection camera systems, adding another layer of technology to support pedestrian awareness around the fleet.
For a busy food manufacturing environment where people, materials and handling equipment operate alongside one another, combining fleet information, compliance monitoring and safety technology provides GCB Cocoa UK with a more connected approach to managing its materials handling operation.
A Complete Materials Handling Solution for GCB Cocoa UK
From narrow-aisle storage and high-level pallet handling to factory-floor transportation and fleet management, the latest project provides GCB Cocoa UK with equipment tailored to the different demands of its Suffolk operation. The combination of three Aisle Master articulated forklifts, six Combilift CS pedestrian stackers and GemOne Sapphire fleet technology creates an integrated solution designed around space utilisation, efficient product movement, operator safety and long-term fleet management.
For Fork Truck Direct, the project demonstrates how understanding the requirements of an individual site can help create a materials handling solution that goes beyond simply supplying a forklift.
Looking to improve materials handling within your warehouse or manufacturing operation?
Contact Fork Truck Direct to discuss your requirements with our team or request a quotation for equipment tailored to your operation.